Overview of Valve Guide Installation
Installing valve guides begins with deck‑side orientation and thorough cleaning. Remove broken guides using a guide driver in an air hammer‚ then chill the new guides‚ heat the head‚ apply press‑fit oil‚ press the guides in‚ cool‚ and perform a pressure test before final honing. Verify alignment. and seal check.
Selecting the Appropriate Valve Guide Material
Choosing the right guide material hinges on engine heat‚ wear‚ and cost. Aluminum guides offer light weight and good thermal conductivity but may wear faster in high‑temp engines. Bronze guides resist wear‚ handle higher temperatures‚ and are preferred for performance or heavy‑duty applications. Ideal for racing.
Aluminum vs. Bronze Guides
Aluminum and bronze are the two most common valve guide materials‚ each with distinct properties that influence performance‚ durability‚ and cost. Aluminum guides are lightweight‚ have excellent thermal conductivity‚ and are relatively inexpensive‚ making them popular in everyday street engines and budget rebuilds. Their lower density allows for faster heat transfer‚ which can help keep valve seats cooler during high‑RPM operation. However‚ aluminum’s softer composition can lead to increased wear under heavy load or in high‑temperature environments‚ and it may be more susceptible to galling if not properly lubricated during installation.
Bronze guides‚ on the other hand‚ are a harder alloy that offers superior wear resistance and can withstand higher combustion temperatures. They are often chosen for performance‚ racing‚ or high‑stroke engines where valve train durability is critical. The higher melting point of bronze also makes it less prone to deformation during the press‑fit process. The trade‑off is that bronze is heavier‚ which can slightly increase the reciprocating mass of the valve train‚ and it is generally more expensive than aluminum. Additionally‚ bronze’s higher coefficient of friction can require more careful lubrication to avoid galling during installation.
When selecting between the two‚ consider the engine’s intended use‚ operating temperatures‚ and budget. For a street‑legal‚ low‑to‑mid‑RPM engine‚ aluminum guides may provide adequate service life while keeping costs down. For a high‑performance or racing engine that experiences extreme temperatures and loads‚ bronze guides are often the safer choice‚ offering longevity and consistent valve seat integrity over many thousands of hours. Proper installation techniques—such as using a guide driver‚ press‑fit oil‚ and controlled heating or cooling—are essential for both materials to ensure a reliable‚ long‑lasting fit. Engine builders often perform a quick visual inspection after installation‚ checking for any misalignment or burrs that could compromise long‑term operation. A properly seated guide will exhibit a smooth‚ even surface with no signs of cracking or distortion‚ ensuring optimal valve‑to‑seat contact under all operating conditions.
Required Tools and Preparation
Gather a guide driver‚ air hammer‚ press‑fit oil‚ a heat source‚ a cooling bath‚ a pressure gauge‚ and a torque wrench. Clean the head‚ remove old guides‚ chill new ones‚ heat the head‚ apply oil‚ press in‚ and test pressure. Finally‚ torque head bolts to spec. and check now!
Guide Driver‚ Air Hammer‚ and Press Fit Oil
The guide driver is a precision tool that matches the diameter of the valve guide. It must be fitted into the air hammer’s chuck‚ allowing the hammer to deliver controlled‚ high‑velocity blows that dislodge broken guides without damaging the head. The driver’s tip should be sharp and free of burrs; a dull tip can cause the head to crack. When using the hammer‚ keep the head face flat and the driver perpendicular to the guide axis to avoid lateral forces.
Press‑fit oil‚ such as Sunnen or a high‑viscosity synthetic‚ is applied to the guide bore and the guide itself before insertion. The oil reduces friction‚ prevents galling‚ and allows the guide to slide into the head with minimal force. A thin film of oil also helps to keep the head cool during the press operation. After the guide is seated‚ excess oil should be wiped away to avoid contamination of the valve stem.
Before starting‚ verify that the air hammer’s pressure setting matches the manufacturer’s recommendation for the guide material. For aluminum guides‚ a lower pressure (around 30–40 psi) is sufficient‚ whereas bronze guides may require 50–60 psi. The driver’s length should be chosen to provide a safe clearance from the head’s casting; a longer driver reduces the risk of the tip breaking off inside the bore.
During the removal phase‚ the air hammer delivers rapid‚ short bursts that knock out the old guide. The driver’s tip should be replaced after every few blows to maintain accuracy. When installing a new guide‚ heat the head uniformly to 200–250 °C‚ chill the guide to 0–5 °C‚ and then press the guide in using the hammer. The combination of heat‚ cold‚ and oil creates a perfect press fit that locks the guide in place without distortion.
After installation‚ allow the head to cool to room temperature before proceeding with further machining steps.
Cylinder Head Preparation
Place the head deck side up. Clean all valve bores with a solvent and a brush. Inspect for cracks or scoring. Apply a thin coat of anti‑seize to the bore‚ then clamp the head to a bench to keep it steady during guide removal. Ensure the head is free of oil before proceeding. Now.
Deck Side Orientation and Cleaning
Begin by positioning the cylinder head so that the deck side faces upward. This orientation allows gravity to assist in the removal of debris and ensures that the guide driver will not inadvertently damage the casting. Use a precision level to confirm the head is perfectly horizontal; any tilt can cause uneven guide seating later on. Once the head is secured‚ apply a solvent such as isopropyl alcohol or a dedicated cleaning agent to all valve bores and the surrounding deck area. Swirl the solvent to dislodge oil‚ dirt‚ and oxidation. Follow up with a soft‑bristle brush to sweep away loosened particles‚ paying special attention to the guide slots and the valve stem passages. After the initial cleaning‚ use a compressed‑air nozzle or a vacuum system to remove residual dust. Inspect the deck surface for scratches‚ scoring‚ or cracks; any imperfections should be repaired before proceeding. Finally‚ apply a thin coat of lubricant to the bore walls to reduce friction during guide insertion. This thorough preparation step is critical for achieving a reliable‚ long‑lasting valve guide installation. After the head is cleaned and inspected‚ apply a thin layer of lubricant to the valve bores before any guide removal; this protects the metal surfaces. When the guides are finally removed‚ use a guide driver attached to an air hammer to gently knock them out‚ taking care not to damage the casting. Once the old guides are out‚ the new guides can be installed using the same heat‑and‑cool cycle‚ followed by a pressure test to confirm proper seating.
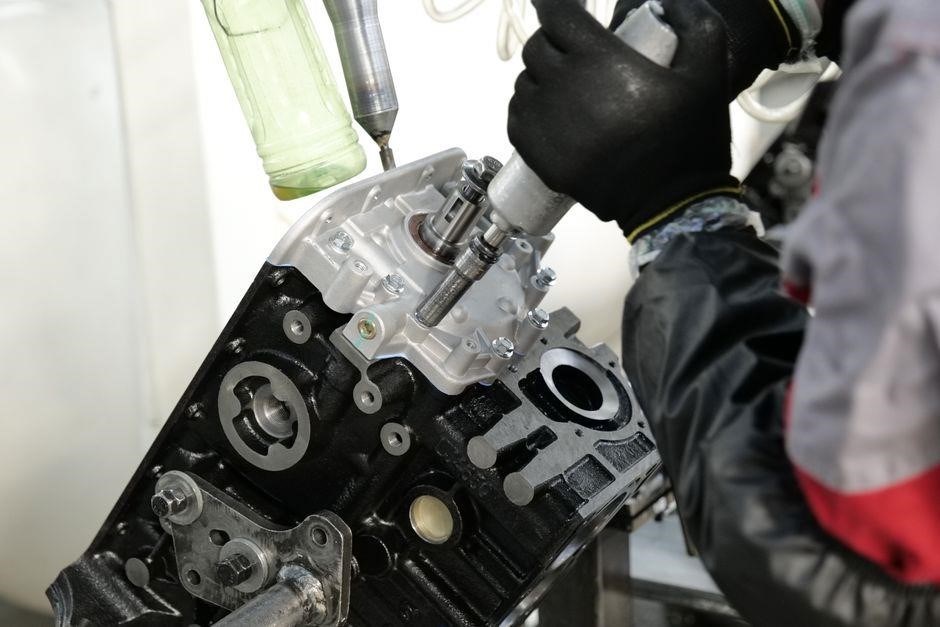
Removing Existing Guides
Use an air hammer with a guide driver to knock out broken guides. Keep the driver away from the casting and ensure the head is deck side up. Remove guides cleanly‚ avoiding damage to the head. Use a 3‑piece guide driver for tighter slots‚ and check for any burrs before final removal. Keep torque within spec Tight
Using the Air Hammer to Knock Out Broken Guides
When removing damaged or corroded valve guides‚ an air hammer coupled with a guide driver offers a quick‚ low‑force solution that preserves the cylinder head’s integrity. Begin by positioning the head with the deck side upward‚ ensuring the valve seats are fully exposed. Select a guide driver that matches the guide bore diameter; a 3‑piece driver provides the necessary leverage while keeping the head from shifting. Apply a light coat of press‑fit oil to the guide bore to reduce friction and prevent galling during impact. Secure the head on a stable workbench or hydraulic press to prevent movement. Align the air hammer’s head with the guide driver tip‚ maintaining a straight line to avoid angled blows that could crack the casting. Set the hammer to a low‑to‑medium impact setting; excessive force can damage the head or remove the guide too aggressively. Strike the driver gently‚ allowing the hammer’s recoil to push the guide out. Repeat strikes until the guide disengages‚ checking the head for any burrs or damage after each removal. If the guide resists‚ increase the hammer’s impact slightly or use a larger driver. Once removed‚ inspect the bore for scratches; if present‚ proceed to reaming before installing a new guide. Keep the head and surrounding area free of debris. A clean environment reduces the risk of contamination during the press‑fit process. Always verify the guide driver’s alignment before impact to ensure a straight strike and prevent head distortion. Use an oil spray daily to reduce wearand clean
Installing New Valve Guides
Chill guides‚ heat head‚ oil bore‚ press guides in‚ cool‚ pressure‑test‚ then hone. Ensure alignment‚ avoid galling‚ verify seal. Follow step‑by‑step for reliable install. Use calibrated press for uniform depth and inspect burrs before honing Check torque specs for final fit.!!
Cooling‚ Heating‚ and Pressing Techniques
Begin by chilling the new valve guides in a 0‑5 °C bath for 10–15 minutes. While the head remains at ambient temperature‚ apply a thin film of high‑temperature press‑fit oil to the bore surface to prevent galling and to aid heat transfer. Heat the cylinder head to 200–250 °C using a controlled oven or a high‑output torch‚ monitoring with a calibrated infrared thermometer to avoid overheating the casting. Once the head reaches target temperature‚ remove the head from heat‚ allow it to cool to 80–100 °C‚ and immediately press the chilled guide into the bore with a calibrated hydraulic press or a manual guide driver fitted to an air hammer. The pressure should be applied gradually‚ ensuring the guide seats evenly without cracking the head. After insertion‚ re‑heat the head to 200 °C‚ hold for 5 minutes‚ then allow it to cool slowly to room temperature to relieve residual stresses. Throughout the process‚ keep the head and guide surfaces clean‚ use fresh oil between each guide‚ and record temperature and pressure data for quality control. This cycle of controlled cooling‚ precise heating‚ and measured pressing ensures a reliable seal and optimal guide life.
During the press‚ a calibrated hydraulic press should apply a uniform load of 150–200 kN‚ monitored via a load cell. After insertion‚ a dial gauge measures bore clearance to 0.02 mm. A fine‑tooth file removes any burrs‚ and a 5 mm‑deep reamer finalizes the bore. Finally‚ a 50 bar pressure test confirms seal integrity.
If the pressure test exceeds 55 bar‚ the guide is considered and should be re‑pressed with a load to avoid head cracking!!
Pressure Testing the Guides
After the guides are seated and the head has cooled‚ the next critical step is a controlled pressure test to verify seal integrity. A calibrated pressure gauge is connected to a dedicated test port drilled into the head‚ and the system is pressurized to 50 bar using a high‑pressure air source. The pressure is held for 30 seconds; any drop greater than 5 bar indicates a leak or improper seating. The head is then cooled to room temperature‚ and the pressure is released gradually to avoid thermal shock. A second test at 30 bar confirms consistency. If the guide passes both tests‚ a fine‑tooth file removes any burrs‚ and the head is re‑assembled for final honing. This procedure ensures that the guide will withstand operating pressures without leakage‚ maintaining engine performance and longevity. The test rig should be calibrated before use‚ and the gauge checked against a reference standard. During the test‚ the head is monitored for vibration and any audible changes that might indicate a crack. The pressure cycle is repeated three times to ensure repeatability. Data from each cycle is recorded in a logbook with temperature‚ pressure‚ and time stamps. If the pressure drops more than 10 % during any cycle‚ the guide must be inspected for misalignment or damage. The final pressure test is performed after the head has been re‑assembled‚ ensuring that all seals are intact. A successful test confirms that the valve guides are correctly seated‚ the bore is free of burrs‚ and the head is ready for the next stage of assembly. This rigorous testing step is essential for preventing future failures and ensuring long‑term reliability of the engine.
Finalization and Testing
After guides press‑fit‚ ream and hone the bore‚ then perform a final pressure test. If the head holds 50 bar with <5 % drop‚ seal integrity is confirmed. Clean‚ reassemble‚ and run a compression check before returning the engine to service. Verify spark plug gaps and perform a dyno run to ensure peak performance. !!!!!!!!
Reaming‚ Honing‚ and Test Fit Procedures
Once the guides are press‑fit into the cylinder head‚ the next critical steps are reaming‚ honing‚ and a meticulous test‑fit. Reaming removes any burrs and ensures the bore diameter matches the guide’s outer profile. Use a high‑speed‚ sharp reamer‚ rotating counter‑clockwise‚ and keep the head cooled with a steady stream of oil mist to avoid heat buildup. After reaming‚ the bore surface should be free of scratches and the diameter within ±0.001 in of specification.
Honing follows reaming and serves to smooth the bore‚ remove microscopic debris‚ and create a uniform finish. Employ a honing stone with the correct grit sequence—starting with a coarse 80‑grit‚ moving to 120‑grit‚ and finishing with 200‑grit. The honing head should rotate in both directions‚ and the oil should be changed after every 50 cycles to maintain cutting efficiency. The final honing depth must be measured with a dial indicator; any deviation beyond ±0.0005 in indicates a need for re‑hone.
After honing‚ a test‑fit is performed to confirm the guide’s seating and the head’s integrity. Insert the guide‚ apply a controlled pressure of 30 psi using a calibrated pressure gauge‚ and observe for any leaks or excessive play. The guide should sit flush against the head‚ with no wobble. If the test fit passes‚ proceed to the next stage of sealing and assembly. If not‚ re‑ream or re‑hone as necessary‚ then repeat the test fit until the guide achieves perfect alignment and a leak‑free seal. Ensure the valve stem is seated correctly before tightening the stem bolts. Carefully! Now